A 6 MW turbine that trips on high bearing metal temperature at two in the morning has usually been telling you something for three weeks, and nobody was reading the trend. Turbine bearing babbitt failure rarely arrives without warning. It arrives after a slow drift that sits comfortably inside the alarm band, and the plant only reacts once the white metal has already smeared.
By that point you are no longer looking at a straightforward bearing shell replacement. You are lifting a casing, sending a journal out for repair, and paying for weeks of bridging diesel, at several times the cost. The gap between those two outcomes is a temperature trend somebody looked at on time.
What happens in a turbine bearing babbitt failure, and why the margin is so thin
Babbitt is soft white metal, usually tin based, cast onto a steel or bronze bearing shell in a layer roughly 0.5 mm to 2 mm thick. It is soft on purpose. It embeds dirt, conforms to small geometry errors, and gives up its own material rather than damaging a shaft journal that costs a hundred times more to fix.
The alloys are covered by ASTM B23, and the tin based grades used in turbine bearings do not fail by melting in normal service. They fail by softening. Fatigue and creep strength drop away well before the solidus, which is why most OEMs alarm near 100°C to 110°C and trip near 115°C to 130°C.
What keeps the babbitt away from the journal is a hydrodynamic oil film, typically 20 to 60 micrometres thick at operating speed on a mid sized turbine journal. Load, speed, clearance, oil viscosity and journal condition all feed into it, and any one of them moving the wrong way closes the gap. A wipe is what happens when that film collapses: the journal touches the babbitt, friction heat goes into a thin layer of soft metal, and the babbitt smears in the direction of rotation. Once smearing starts, the geometry that generated the film is gone, so the process accelerates.
Two operating states have no hydrodynamic film at all. Run up and coast down pass through boundary lubrication, and turning gear or slow roll is boundary lubrication by definition. That is why heavy rotors have a jacking oil, or lift oil, system that floats the journal hydrostatically at low speed.
If your bearing temperature trends, shaft centreline data and oil analysis results have never been reviewed together by an engineer, that review is cheap next to what it finds. Request a technical proposal and we will scope the assessment before anything is opened.
Warning signs of a babbitt wipe, in the order they actually appear
The first indicator is bearing metal temperature, measured by an RTD or thermocouple embedded in the babbitt a few millimetres below the running surface, near the trailing edge of the loaded arc or pad. The absolute number matters less than the trend. A rise of 6°C to 10°C over several weeks at unchanged load, oil inlet temperature and ambient is a genuine signal even if the reading sits well below alarm.
The second is the gap between oil inlet and bearing drain temperature. It is blunter than the embedded RTD because it averages across the whole bearing, but a widening differential at constant flow says more heat is being generated than before.
The third is shaft centreline position, the most underused diagnostic on most plants. The DC gap voltage from the X and Y proximity probes tells you where the journal is sitting inside the bearing. As babbitt is lost the shaft drops within the clearance, and that movement often shows up before vibration amplitude does anything interesting.
The fourth is vibration behaviour rather than vibration level. Watch for a change in 1x amplitude together with a phase shift, and for subsynchronous energy in the 0.38 to 0.48 times running speed band, which points at oil whirl in a bearing that has lost load or opened up its clearance. Our note on steam turbine high vibration works through the diagnostic sequence.
The fifth is the oil. Rising tin, antimony, copper or lead on spectrographic analysis, a climbing particle count, or metallic debris on the magnetic plug and in the filter all point at bearing surface loss. Sampling frequency matters more than test sophistication, and turbine lube oil analysis covers what to test and how often.
Worked example (hypothetical): a 1.6 MW back pressure steam turbine running continuous shift work. Gland steam leakage into the front bearing pedestal pushes water content in the oil to around 1,800 ppm over several months, and nobody samples because the machine keeps running and the temperature stays inside alarm.
Water plus heat on tin babbitt produces tin oxide corrosion, a hard black scab that destroys the running surface and then acts as an abrasive. In that case the front journal bearing wipes around fourteen months after commissioning. Rebabbitting both shells, plus an oil system drain and flush, runs to several times the cost of the oil sample that would have caught the water ingress months earlier, and the outage costs several days of lost production.
Root causes of babbitt bearing wipe on steam and gas turbines
Lubrication supply failure is the fastest and most brutal cause. A main pump losing suction, an emergency pump that fails to pick up on changeover, a filter that clogs while its bypass sticks shut, a blocked supply orifice, or air entrainment from a low reservoir level will starve the bearing within seconds to minutes. Emergency and DC backup pumps that are never tested under load are a recurring finding.
Viscosity loss is slower and just as damaging. Fouled oil coolers, high oil inlet temperature, the wrong ISO grade after a top up, or dilution by fuel or water all thin the film. Turbine systems generally run ISO VG 32 or VG 46, and mixing grades across a fleet is a common site level error.
Contamination works two ways. Water corrodes and reduces film strength. Hard particles, whether silica left by an inadequate flush, weld spatter from a rebuild, or wear debris from elsewhere in the train, score the journal and embed in the babbitt.
Mechanical and dynamic causes need engineering rather than housekeeping. Coupling misalignment, pipe strain on the turbine casing, soft foot, foundation settlement and differential thermal growth all change how load sits across the bearings. A bearing unloaded by misalignment is a candidate for oil whirl, which can lock onto the rotor first critical speed as oil whip and destroy the babbitt quickly.
Electrical discharge is often missed. Shaft voltage from residual magnetism, wet steam friction on the blading, or a failed grounding brush drives current through the oil film, producing pitting and eventually the fluted surface that shows up at strip down. The brush is a cheap item frequently found worn out or disconnected.
Thrust bearings fail for their own reasons. On steam turbines, deposits on the blading raise stage pressure drop and increase axial thrust, and loss of condenser vacuum does the same. Water induction into a hot casing causes distortion and rubbing that no bearing design absorbs.
A previous repair can also be the root cause. Babbitt bonded poorly to the shell, a bond line never checked by ultrasonic testing, or a layer cast thicker than design will fatigue and lift out under load however good the oil is.
Worked example (hypothetical): a 6 MW gas turbine generator shuts down normally for inspection. Lift oil supply is lost during a pump changeover and the fault is not clearly annunciated, so the turning gear keeps rolling the rotor for around 40 minutes with no hydrostatic lift. Both journal bearings wipe and one journal scores to about 0.15 mm depth.
In that case the rotor has to come out. Journal repair by thermal spray and regrinding, new bearings, alignment and recommissioning is a major project, and the unit is off line for weeks. Bridging on diesel while the gas turbine is down adds a large fuel differential against the gas it would otherwise burn, easily several times the annual cost of maintaining a tested DC backup lift oil pump that would have prevented the trip. If your lift oil and emergency pump changeovers have never been proved under load, book a plant assessment and have it witnessed properly.
Repair options after a wiped turbine bearing, and what each one costs
The first decision is not which repair, it is whether the journal is damaged. A light wipe on an undamaged journal is a bearing job. A scored journal is a rotor job, and the cost and outage window change by an order of magnitude. That determination needs the bearing opened and the journal measured for ovality, taper, surface finish and hardness.
The table below is indicative for a 5 MW to 15 MW class steam or gas turbine with journal diameters roughly 200 mm to 350 mm, at a Nigerian site with reasonable access. Figures move with journal size, parts scope, exchange rate and whether work is done locally or abroad. Treat it as a planning envelope, not a quotation.
| Repair option | When it applies | Outage window | Main risk |
|---|---|---|---|
| In situ inspection, hand scrape and blue | Very light wipe, geometry intact, journal clean | 2 to 4 days | Treating a symptom while the root cause remains |
| Rebabbitt existing shell | Babbitt lost, shell and journal serviceable | 10 to 20 working days per shell | Poor bond line if not ultrasonically tested |
| Rotable spare shell exchange | Spare already held and certified | 3 to 5 days | Capital tied up in stock |
| New OEM journal bearing | Shell damaged, or design change required | 12 to 30 weeks lead time | Lead time dominates the schedule |
| Journal repair, thermal spray and regrind | Journal scored beyond polishing limits | 4 to 8 weeks, rotor out | Requires rotor removal and a machine shop |
| Tilting pad conversion with rotordynamic study | Repeat instability or chronic oil whirl | 6 to 12 months engineering plus parts | Only justified if instability is proven |
Cost moves with journal size, parts scope and whether work is done locally or abroad, so treat the table as a scoping guide rather than a quotation.
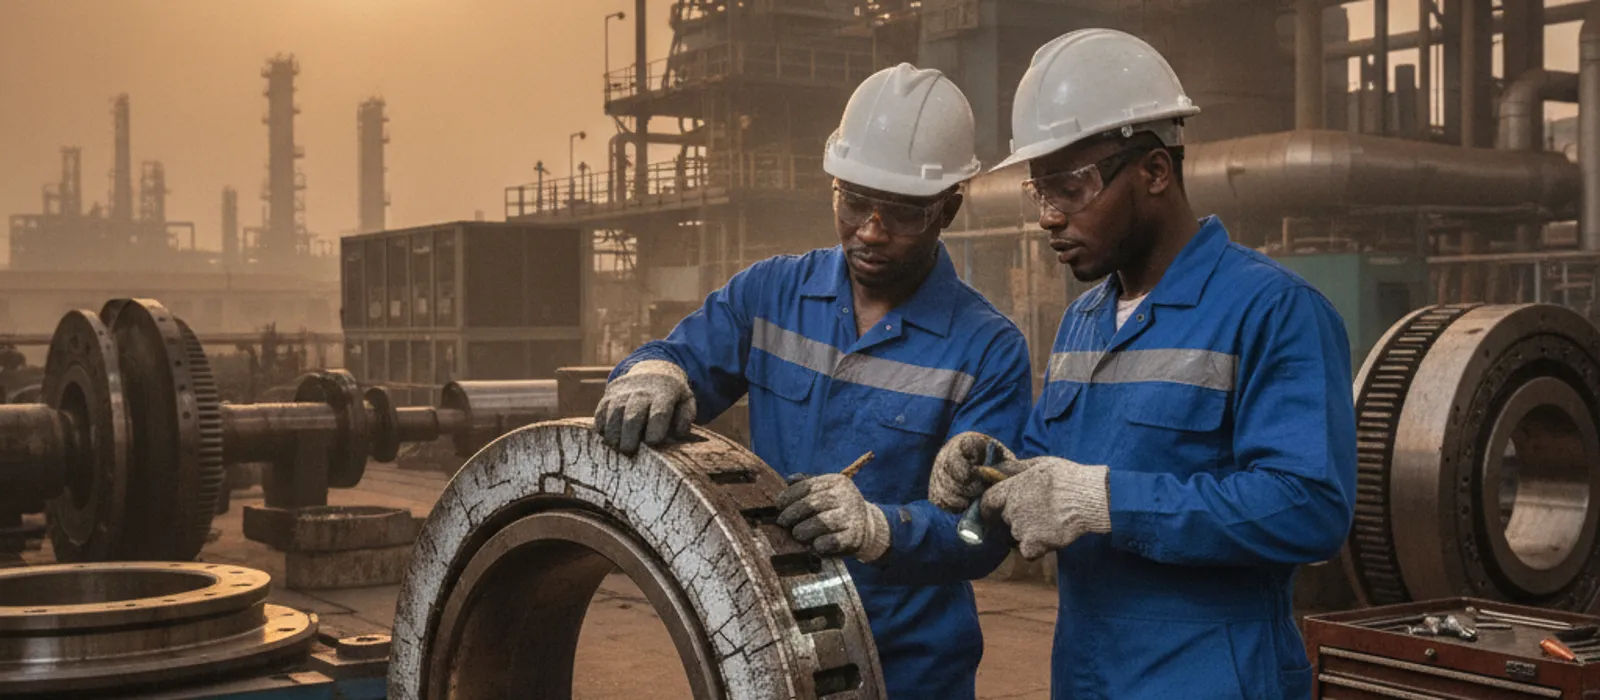
Rebabbitting is not a general workshop job. The old metal is stripped, the shell is cleaned and tinned to create the bond layer, the babbitt is cast, and the bore is machined and scraped to the specified clearance and contact pattern. The bond line then needs ultrasonic testing and the surface needs dye penetrant inspection. Skip those checks and you have bought a bearing that will fatigue out under load.
Worked example (hypothetical): a 12 MW condensing turbine. A wiped shell is rebabbitted by a general engineering workshop with no bond line testing and no check on journal surface finish. It wipes again five months later, and the second event costs an order of magnitude more, including a fresh outage and journal repair.
Lead time is the other planning trap. OEM bearings and thrust assemblies routinely take three to seven months door to door once shipping and clearance are counted, as set out in turbine spare parts lead time. Where a day of lost production is expensive, holding a certified rotable shell is usually the better trade, and plant downtime cost per hour shows how to work that number for your own plant.
Preventing the next turbine bearing babbitt failure
Oil cleanliness targets should be written down and measured, not assumed. Most turbine lube systems should be held near ISO 4406 16/14/11 or better, with water content below 100 to 200 ppm depending on the OEM specification. After any oil system work, flush to a measured cleanliness target rather than until the oil looks clean.
Instrumentation is where most sites are quietly exposed. Two temperature elements per bearing rather than one, X and Y proximity probes at 90 degrees, thrust position probes, and alarm and trip setpoints that have been proved rather than inherited from a commissioning file. Check that trend data is stored at a useful interval, because a monthly snapshot will not show you a six week drift.
Be clear about what condition monitoring does. Temperature, vibration and oil data will tell you that something is changing and often what class of problem it is. They will not measure babbitt thickness or bond integrity, and they do not remove the need for physical inspection at the OEM interval. What they buy is time between a fault starting and you knowing about it.
Alignment discipline matters as much as lubrication. Hot alignment checks, pipe strain checks at the turbine flanges and catenary settings on multi bearing trains all decide how load sits across the bearings. That is measurement work with proper tooling, not a visual judgement, and it belongs in the scope whenever a casing has been opened. It sits inside the wider rotating equipment services scope rather than being a turbine only issue.
ISO 7902-3 sets out permissible operational parameters for hydrodynamic plain journal bearings and gives you a defensible basis for acceptance criteria in a tender or repair specification. On steam machines this work is normally folded into the broader steam turbine overhaul scope, where clearances, alignment and oil system condition are addressed together.
Say plainly what needs specialists. Casing lifts, rotor removal, journal machining, clearance setting and rotordynamic assessment require calibrated tooling, correct rigging and a qualified turbine engineer on site. If your unit is showing a drifting bearing temperature or an unexplained shaft position change, request a technical proposal before the trend closes the decision for you.
Frequently Asked Questions
Can a wiped babbitt bearing be repaired in place, or must the rotor come out?
It depends on how far the wipe went and on the condition of the shaft journal. A light wipe on a horizontally split bearing with an undamaged journal can often be handled by rolling out the lower half, fitting a repaired or spare shell and rechecking clearances, without lifting the rotor. Once the journal is scored beyond polishing limits, or the wipe has caused a rub elsewhere in the machine, the rotor has to come out for machining and inspection. That decision should follow measurement of the journal, not a visual assessment.
What bearing metal temperature should trigger action?
Work from your OEM setpoints rather than a general rule, because they depend on bearing design, load and oil grade. As a guide, many industrial turbines alarm between 100°C and 110°C and trip between 115°C and 130°C. The more useful trigger is the trend: a sustained rise of 6°C to 10°C at constant load, oil inlet temperature and ambient deserves investigation even while the reading is still below alarm.
How long does rebabbitting take, and can it be done locally in Nigeria?
Rebabbitting a journal shell typically takes 10 to 20 working days per shell once the shell is at the workshop. Local capability exists, but capability varies widely, and the difference shows up in bond quality rather than appearance. Insist on tinning procedure records, ultrasonic bond line testing, dye penetrant inspection and a dimensional report against the OEM clearance before the shell is accepted. Compare that turnaround against OEM parts lead times of three to seven months when deciding your route.
Does a babbitt wipe always damage the shaft journal?
No, and that is the point of the material. Babbitt is intended to be sacrificial so the journal survives, and in many light wipes the journal cleans up with polishing and is returned to service within tolerance. Severe wipes, contamination by hard particles, or continued running after contact starts will score or heat check the journal. Only measurement of ovality, taper, surface finish and hardness will tell you which case you have.